1.5KW EC Motor for Large-Scale Poultry Tunnel Ventilation Systems
High-torque 1.5KW EC brushless motor designed for large-scale poultry tunnel ventilation. Features stepless speed regulation, IP66 protection, and seamless smart control integration to fix uneven airflow and high power consumption on commercial livestock farms.
Product description
1.5KW EC motor for poultry fans, commercial tunnel ventilation motor, high torque livestock exhaust fan motor, energy saving brushless fan motor for large barns, stepless speed tunnel ventilation motor, heat stress prevention ventilation motor for commercial poultry farm, low maintenance livestock fan motor for Southeast Asian farms
For commercial poultry and swine integrators operating large-scale tunnel-ventilated barns, ventilation performance is no longer a basic operational requirement — it is the core factor that determines flock uniformity, feed conversion ratio, and overall farm profit margin. Many mid-to-large commercial farms still rely on traditional single-speed induction fan motors, which have long been the hidden cause of unstable barn environments and excessive operational costs. Unlike small farms that only need basic air exchange, large-scale tunnel ventilation systems require consistent airflow pressure, adjustable wind speed zoning, and long-term stable continuous operation, demands that ordinary fixed-speed motors simply cannot meet.
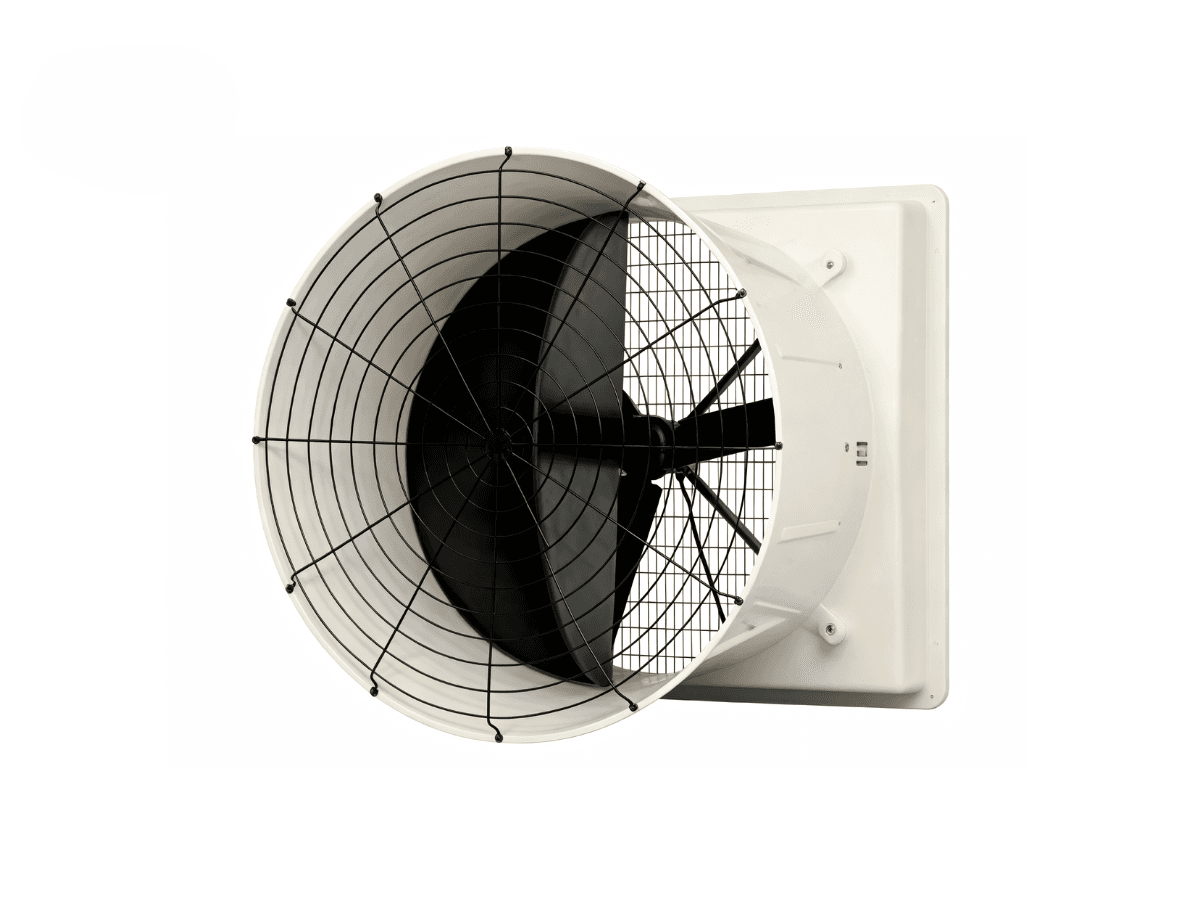
The HNRK160 1.5KW EC motor is professionally engineered for standard commercial livestock tunnel ventilation scenarios. It fills the performance gap between low-power small-farm motors and heavy-duty industrial motors, serving as the most cost-effective power solution for multi-row tunnel fan arrays in large broiler houses, layer breeding barns, and intensive swine finishing facilities. Tailored to the pain points of commercial farm ventilation — uneven long-distance airflow, seasonal ventilation mismatch, high energy waste, and frequent motor burnout — this brushless EC motor delivers precise, stable, and energy-efficient ventilation power for large-scale breeding environments.
Why Traditional Fan Motors Fail on Commercial Tunnel Ventilation
Most large poultry farms encounter identical ventilation dilemmas after long-term operation, all stemming from the inherent defects of conventional fixed-speed motors. In standard tunnel ventilation design, fresh air enters from one end of the barn and hot humid air is exhausted from the opposite end, forming a longitudinal airflow loop. Traditional motors run at a constant maximum speed 24 hours a day, leading to two extreme operational problems that severely restrict farm production efficiency.
First, fixed-speed operation causes severe airflow imbalance in long barns. In barns exceeding 60 meters in length, constant high-speed operation creates excessive wind pressure near the exhaust fans, resulting in strong airflow at the tail end while forming obvious dead air zones at the air inlet side. This uneven airflow distribution leads to temperature differences of 3–4℃ between the two ends of the barn, alongside accumulated ammonia and moisture in low-airflow areas. Local high temperature and humidity cause inconsistent chicken growth rates, increased small-sized broiler ratios, and reduced eggshell quality in layer flocks, directly lowering batch output benefits.
Second, non-stop full-speed operation generates massive unnecessary energy consumption. Commercial livestock ventilation requires dynamic adjustment according to external temperature, bird age, and flock density. During cool nights, rainy seasons, and young bird breeding periods, barns only need low-volume air exchange to eliminate moisture and harmful gases. However, fixed-speed motors cannot adjust output, resulting in long-term idling power waste. For large farms equipped with 20–40 tunnel fans, this ineffective power consumption accumulates into tens of thousands of dollars of additional electricity costs every year, becoming a major hidden operational burden.
In addition, traditional induction motors have weak environmental adaptability. The high humidity, ammonia corrosion, and floating feed dust inside commercial barns easily cause internal coil aging and short circuits. Frequent startup and shutdown under unstable rural grid conditions further shorten motor service life, leading to frequent equipment maintenance and unexpected fan shutdowns. Temporary ventilation failures often trigger large-area heat stress in flocks, bringing irreversible economic losses to commercial breeding projects.
Core Advantages of 1.5KW EC Motor for Commercial Tunnel Ventilation
The HNRK160 1.5KW EC brushless motor completely abandons the working mode of traditional induction motors, relying on advanced electronic commutation technology and stepless speed regulation logic to perfectly match the dynamic ventilation needs of large-scale commercial barns. Its core value lies in converting “fixed mechanical ventilation” into “intelligent demand-based ventilation”, solving the pain points of uneven airflow, high energy consumption, and poor stability in commercial tunnel systems from the root cause.
The most prominent advantage is precision stepless speed regulation (200–600RPM) exclusive for tunnel ventilation. Different from the single fixed gear of ordinary motors, this EC motor supports smooth linear speed adjustment within the full range. Farm environmental controllers can automatically adjust fan speed in real time based on indoor temperature, humidity, ammonia concentration, and bird growth cycle. In hot summer daytime, the motor runs at high speed to maximize air volume, forming a 2.5–3.5m/s tunnel wind speed to accelerate heat dissipation and eliminate flock heat stress. In cool nighttime and winter seasons, it maintains low-speed stable operation to ensure minimum ventilation requirements, avoiding cold stress caused by excessive air exchange while continuously discharging harmful gases.
In terms of energy saving, the brushless structure eliminates carbon brush friction loss and no-load power consumption of traditional motors, achieving 40–60% comprehensive energy efficiency improvement. For large commercial farms with long-term continuous ventilation needs, the energy-saving benefit is extremely obvious. After actual testing on Southeast Asian tropical breeding farms, replacing traditional motors with 1.5KW EC motors can save an average of 40–50% of ventilation electricity bills every year, and the equipment investment cost can be fully recovered within 1–2 breeding cycles, bringing stable long-term cost reduction benefits for farm operations.
Industrial-Grade Durability Adapted to Harsh Commercial Barn Environments
Commercial livestock barns have extremely harsh operating conditions, and equipment durability directly determines the stability of farm production. The HNRK160 1.5KW EC motor adopts a fully enclosed industrial-grade design, targeting the high humidity, ammonia corrosion, and dust pollution of large-scale breeding environments, with comprehensive performance upgrades in protection level and structural stability.
It is equipped with IP66 full dustproof and waterproof protection and F-class high-temperature resistant insulation materials. The fully sealed shell structure completely isolates internal circuits from external humid air, ammonia corrosive gas, and floating feed dust, effectively preventing coil aging, short circuits, and motor jamming caused by environmental pollution. Whether it is the high-temperature and high-humidity tropical climate all year round or the humid and cold rainy seasons in subtropical regions, the motor can maintain 24-hour continuous stable operation without frequent failures.
Moreover, the brushless maintenance-free design greatly reduces farm operational and maintenance costs. Traditional motors require regular replacement of carbon brushes, cleaning of dust and oil stains, and inspection of circuit aging, consuming a lot of labor time and maintenance costs every year. The 1.5KW EC motor has no wearable carbon brush components, realizing zero daily maintenance. It can operate stably for a long time in high-intensity working scenarios, avoiding production interruptions and flock health risks caused by equipment maintenance and failure shutdowns, which is very suitable for unattended large-scale commercial breeding bases.
Smart System Integration for Modern Precision Breeding
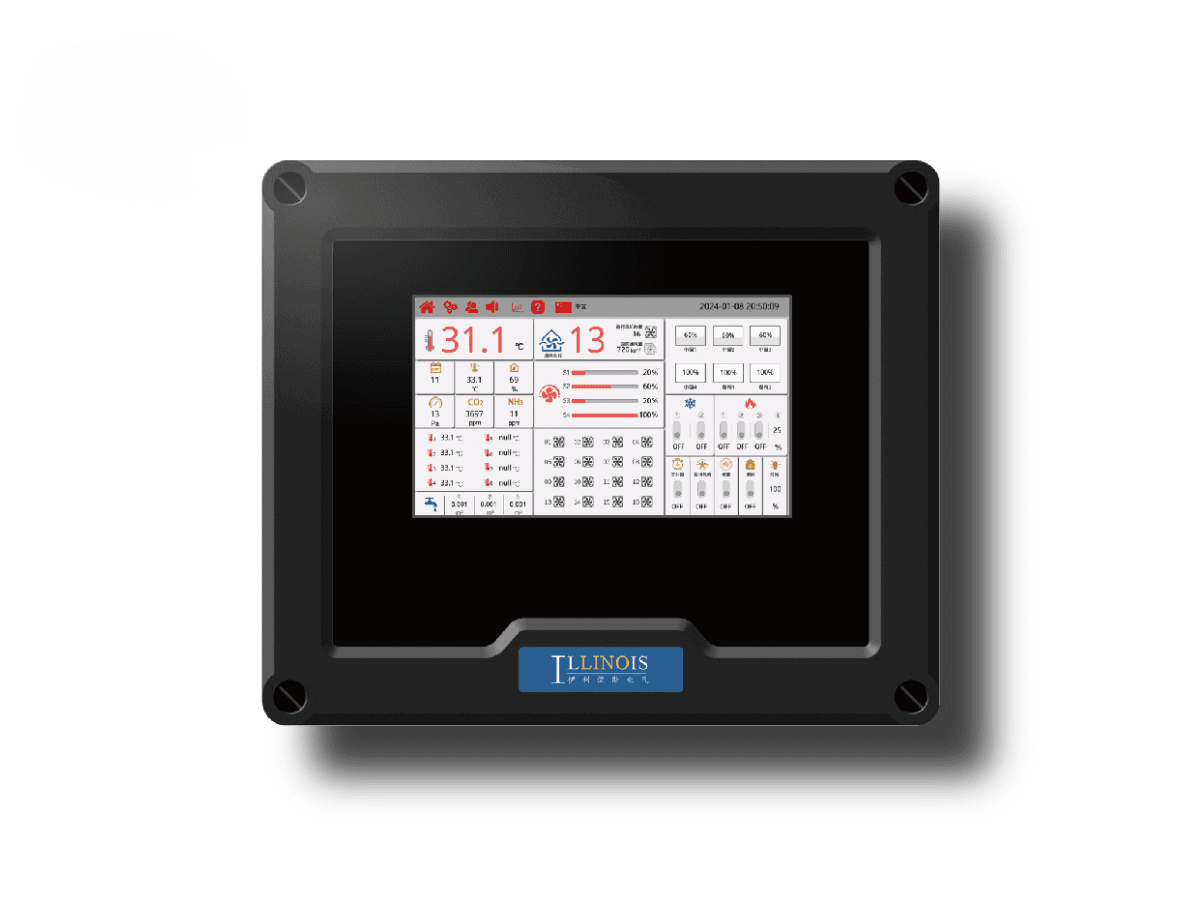
Modern large-scale poultry farming has fully entered the era of intelligent environmental control, and single equipment performance can no longer meet production needs. The HNRK160 1.5KW EC motor supports 0–10V analog signal linkage control, which can be perfectly matched with all mainstream livestock environmental controllers, temperature and humidity sensors, and ammonia gas detection equipment on the market, realizing fully automatic closed-loop ventilation management.
During the breeding process, when the sensor detects that the indoor temperature rises or ammonia concentration exceeds the standard, the system automatically increases the EC motor speed to expand ventilation volume and quickly discharge hot air and harmful gases. When the environmental data returns to the safe range, the motor automatically reduces speed to maintain a balanced microclimate. This intelligent dynamic adjustment mode completely eliminates the errors and delays of manual fan adjustment, ensures that the barn environment is always in the best breeding state, effectively improves flock feed conversion rate and growth uniformity, and reduces mortality and veterinary costs caused by environmental fluctuations.
This strong compatibility also makes it the preferred upgrade solution for old barn renovation projects. Many built large-scale farms have complete environmental control systems but are limited by outdated fan motors, unable to achieve precise ventilation. Directly replacing with 1.5KW EC motors does not need to modify the original circuit and control system, realizing low-cost intelligent upgrading of ventilation systems, helping old farms quickly improve production efficiency and reduce operating costs.
Exclusive Application Scenarios & Commercial Value
The 1.5KW high-torque EC motor is specially positioned for medium and large commercial tunnel ventilation systems, with extremely high scenario matching and cost performance. It is neither overconfigured and wasteful like high-power 2.2KW motors nor insufficient in power like small 0.5KW motors, and is the most widely applicable power model for standard large poultry and pig barns.
It is widely used in large closed broiler breeding barns, commercial layer cage houses, intensive pig finishing barns, and supporting ventilation equipment for agricultural and animal husbandry industrial parks. For Southeast Asian breeding markets with unstable power grids and high annual temperature, its wide voltage adaptation performance and anti-interference design can effectively resist grid voltage fluctuations, ensuring that the ventilation system will not stop running due to voltage instability, protecting flock safety during peak heat waves.
From the perspective of long-term farm operation, upgrading to 1.5KW EC motors can form a multi-dimensional value improvement: stabilize barn microclimate to reduce flock stress and mortality, optimize ventilation efficiency to improve feed conversion, reduce manual maintenance frequency to save labor costs, and cut invalid power consumption to reduce operating expenses. For commercial breeding enterprises pursuing standardized and refined management, it is an essential core equipment to improve overall farm profitability.
If your large-scale poultry or swine farm is still troubled by uneven tunnel ventilation, high power consumption, and frequent motor failures, upgrading to the HNRK160 1.5KW energy-saving EC motor is the most efficient and cost-effective solution. We support customized voltage, speed, and structural specifications for different farm scenarios, and provide complete installation guidance and technical after-sales services. Contact our professional team now to get exclusive commercial farm ventilation upgrade solutions and bulk quotation support.